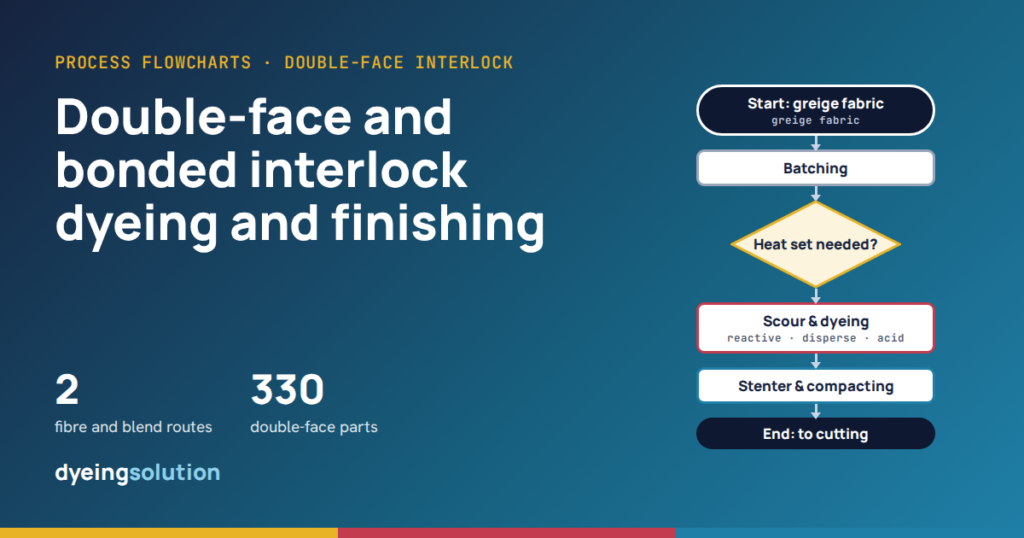
Double-face interlock carries a different yarn on each face, and most of it in our records is polyester-rich with elastane. Here is the route for each fibre, from greige fabric to the cutting table.
At a glance
330Parts in our records
220Median required GSM
65%Within GSM tolerance
69%CVC double-face heat set
Double-face (bonded) interlock is an interlock-based double knit in which each face can be knitted from a different yarn, for example polyester on one face and cotton on the other, held together by tuck stitches. It is thicker and more stable than plain interlock and is used for sportswear, jackets and structured tops.
| Type in our records | Parts |
|---|---|
| Bonded Interlock | 170 |
| L/Bonded Interlock | 78 |
| Y/D Bonded Interlock | 17 |
| Double Face Interlock | 10 |
| Yd Bonded Interlock | 9 |
| L/Double Face Interlock | 8 |
| Ly Bonded Interlock | 5 |
| L/ Double Face Interlock | 5 |
By fibre: what our records show
| Fibre or blend | Parts | Median required GSM | Within ±5% GSM | More than 5% light | Median length shrinkage | Median width shrinkage | Heat set |
|---|---|---|---|---|---|---|---|
| CVC / PC | 262 | 190 | 66% | 27% | 5% | 3% | 69% |
| Polyester-viscose | 41 | 330 | 56% | 21% | 4% | 2% | 73% |
CVC and PC make up most of this fabric: 262 of 330 parts, and 66% of them finish within GSM tolerance.
What is on each face
- Each face of double-face interlock can carry a different fibre. When one face is polyester and the other is cotton, both parts are dyed.
- The two faces can then show two different shades. How it is dyed depends on the fabric construction, how the fabric was made, and what the buyer requires.
Why most of it is heat set
- Bonded interlock is a design type whose stability is not good. The binding is often polyester, or a separate binding yarn, so it must be heat set.
- Bonded interlock usually has Lycra inside as well. That is why about 70% of it in our records is heat set. Double-face is the same.
The sequence before the dyeing machine
Every chart below follows the same sequence before dyeing. Steps a fabric does not need simply drop out; they are drawn dashed.
- Greige inspection, then batching. A fabric that stays a tube is turned inside out here.
- If it needs heat setting, singeing or mercerising: slitting first. None of these is ever done on a tube.
- If it needs heat setting: heat setting in open width.
- If it needs singeing: singeing in open width, after checking the flame cannot damage the fabric.
- If it is mercerised: mercerising, then drying.
- If the fabric was opened: back sewing, to make it a tube again with the face side inside (the loop side, for terry).
- Loading into the dyeing machine, then scouring, bleaching and dyeing, single part or double part as the fibre needs.
Flowcharts by fibre
CVC / PC double-face and bonded interlock
In our records: 262 parts, 66% within GSM tolerance, median length shrinkage 5%, heat set 69%. Full process: CVC / PC dyeing process.
Dyeing and finishing: CVC / PC double-face and bonded interlock
Polyester-viscose double-face and bonded interlock
In our records: 41 parts, 56% within GSM tolerance, median length shrinkage 4%, heat set 73%. Full process: Polyester-viscose dyeing process.
Dyeing and finishing: Polyester-viscose double-face and bonded interlock
Textile engineer with 14+ years in dyeing and fabric development. He writes every guide on Dyeing Solution from real production work. Full profile