A step-by-step development guide for cotton, Lycra and yarn-dyed interlock: structure, yarn, gauge, stitch length, dyeing and finishing, holding GSM and shrinkage, and testing, built on our real development records.
At a glance
887interlock entries in our register
-3.1%median finished vs required GSM
+10.6%median GSM rise after the wash test
17 of 37shrinkage lab results that failed
Interlock is the knit buyers pick when they want single jersey comfort with a fuller, smoother and more stable hand, for baby wear, premium T-shirts, leggings, sleepwear, dresses and school wear. It looks plain on both sides, yet it is a double knit made on two sets of needles, with two feeders building each course. So development differs from single jersey: the fabric is heavier for the same count, needs finer yarn for the same gauge, and its weight and shrinkage are harder to hold in finishing. This guide follows the route from yarn to a tested and approved interlock, using real figures from our development records: 887 interlock entries in our fabric register (cotton, Lycra interlock and yarn-dyed interlock) and 26 interlock test reports from our lab reports. Where a value comes from general practice rather than our records, it is marked as typical. If you are new to knit development, start with the single jersey fabric development guide.
What interlock is
Structure: two 1×1 ribs locked together
Interlock is a weft knitted double knit. It is made on a circular machine with two needle beds: the cylinder, whose needles stand vertically, and the dial, a flat plate above it whose needles move horizontally. On an interlock machine the dial needles stand directly opposite the cylinder needles. This is called interlock gating. On a rib machine the two sets are staggered instead.
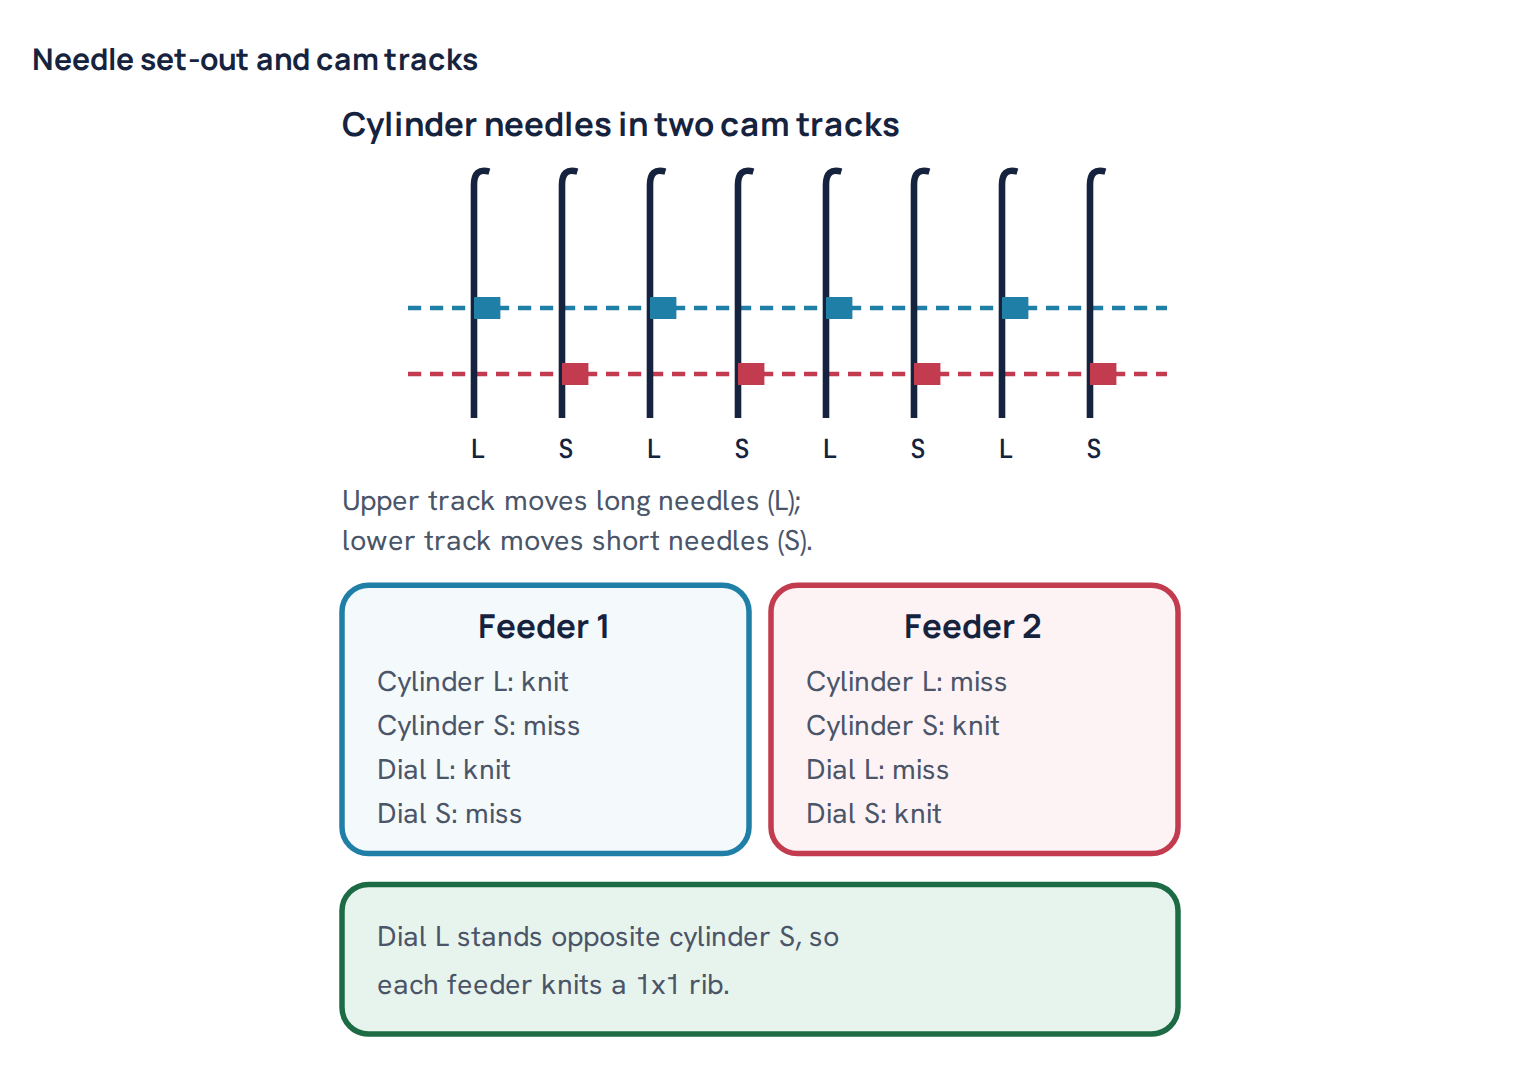
Each bed carries two kinds of needles, set out alternately: long needles and short needles. Their butts run in two different cam tracks, so the cams can make the long needles knit while the short needles stay out of work, and the other way round. A dial long needle stands opposite a cylinder short needle, and a dial short needle opposite a cylinder long needle.
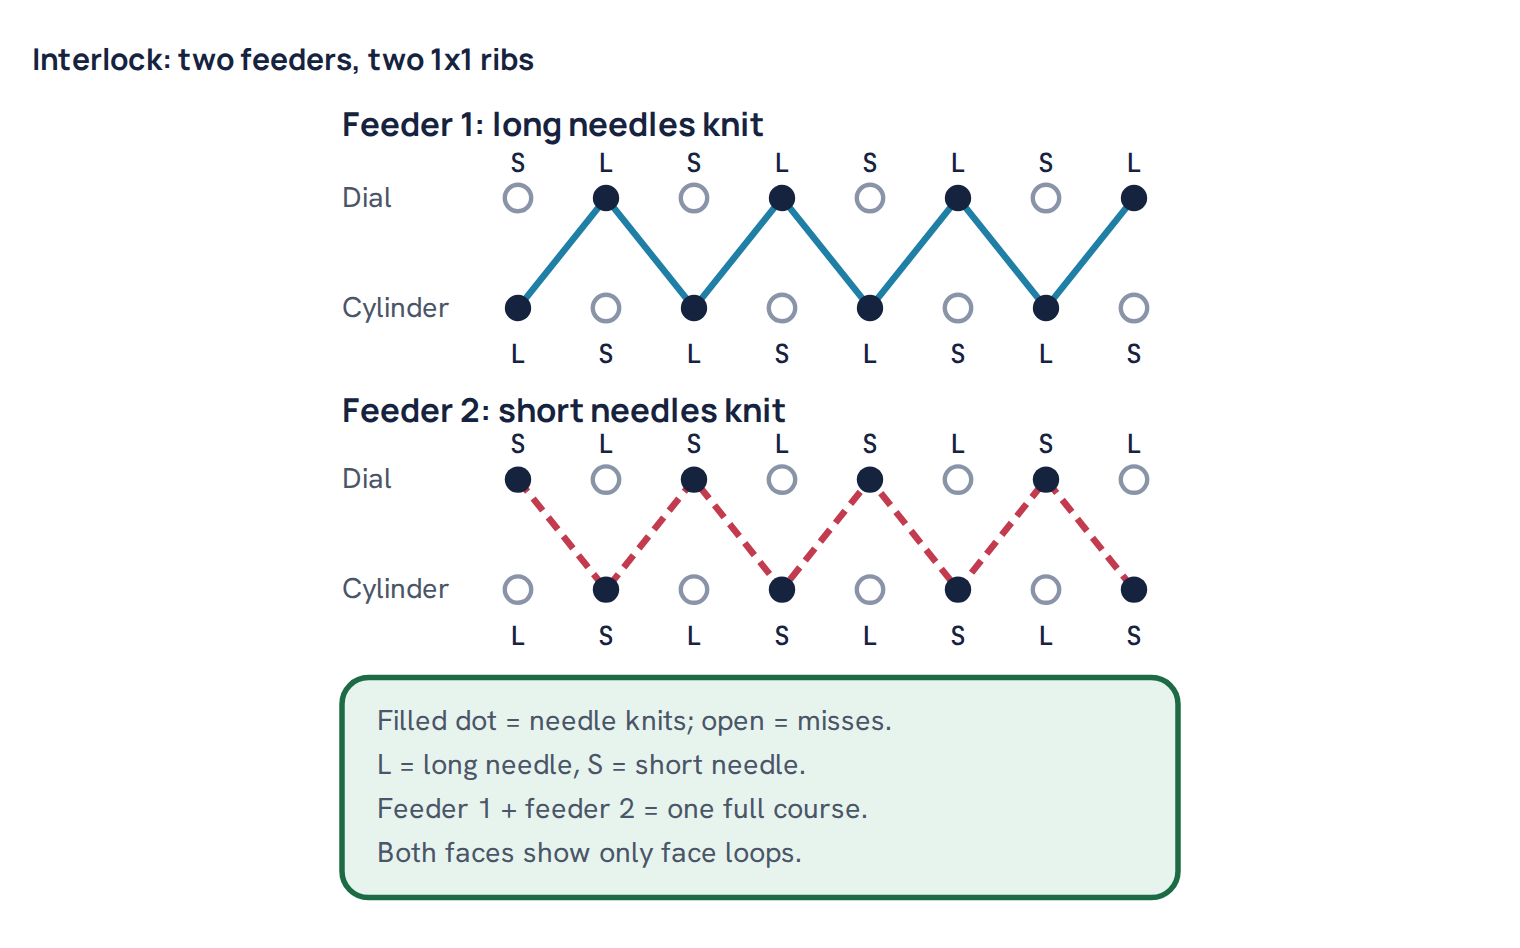
- Feeder 1 knits on the long needles of both beds. Because these needles alternate between the two beds, feeder 1 knits a 1×1 rib.
- Feeder 2 knits on the short needles of both beds, making a second 1×1 rib in the gaps left by the first.
- The two ribs cross each other between the beds and lock together. That is where the name comes from. One complete interlock course therefore needs two feeders.
A wale is a vertical column of loops, a course a horizontal row. Each face of interlock shows a full set of wales, lying exactly behind those of the other face.
Why interlock is smooth on both sides and stable
In a 1×1 rib, each side shows face loops with back loops sunk between them. In interlock the second rib fills those sunk places with its own face loops. Each side therefore shows only face loops, the neat V columns of a jersey face, and the back loops are hidden inside. Turn it over and it looks the same: a balanced, two-faced fabric.
- No edge curl. The loops on both sides pull equally, so cut edges lie flat, which makes slitting, stenter feeding and cutting easier.
- Low spirality. The balanced structure resists yarn twist torque far better than single jersey.
- Stable and less extensible. The two ribs hold each other, so interlock stretches less in width than a 1×1 rib and does not ladder easily. It can be unravelled only from the end knitted last.
- Thick and heavy for its count. Interlock has loops on both beds, so for the same count and stitch length it holds roughly twice the yarn per square metre of single jersey. Interlock is therefore knitted with finer yarns than jersey of the same weight.
- Full handle and good cover. Dense, opaque and smooth, it prints well.
Variants in our register
Our register lists interlock under several names: plain interlock, Lycra interlock and yarn-dyed interlock. By fibre, 670 of the 887 entries are 100% cotton, 138 are CVC or PC (cotton/polyester), 24 are CVC or PC with elastane, 35 are cotton with elastane and the rest are other fibres. The main variants are:
- Cotton interlock. The bulk of the work. Usually combed yarn, piece-dyed with reactive dyes. Some entries are also flagged as mercerised (94 entries) or singed (93 entries), which gives a cleaner, more lustrous face.
- Lycra (elastane) interlock. Bare elastane is fed with the cotton or blend yarn for stretch and recovery. It is used for leggings, fitted tops and dresses. It needs heat setting.
- CVC and PC interlock. Cotton/polyester blends, which shrink less and keep their shape better, but need a disperse dyeing step for the polyester part.
- Yarn-dyed interlock. Knitted from dyed yarns, often in stripes. The fabric is usually washed and finished, not piece-dyed, so shrinkage and fastness depend on how the yarn was dyed.
Development inputs
Read the buyer’s request carefully
Write every requirement in one place before choosing yarn. For interlock, the important items are:
- Finished GSM and its tolerance, often ±5%. The main cotton constructions in our records are required at 180 to 240 GSM.
- Finished width, open width or tubular. All interlock in our register is finished open width.
- Composition, including the exact elastane or polyester share, because fibre content is tested against the label.
- Yarn quality: combed, compact, organic, recycled or certified yarn where named.
- Shade and light source; whites and pastels carry a yellowing risk.
- Wash care, because it sets the shrinkage test conditions.
- Test requirements: dimensional stability, GSM, spirality, bursting strength, pilling, colour fastness, pH, fibre content and, for whites and pastels, phenolic yellowing.
Choosing the yarn
Count. Interlock uses finer counts than single jersey at the same gauge, because two beds of loops share the weight. In our records the common combinations are 36/1 and 40/1 Ne cotton on 24 gauge for about 215 to 240 GSM, and 50/1 Ne on 28 gauge for about 180 GSM. A coarser count raises GSM; a finer count lowers it and gives a smoother, more refined surface.
Combed, compact or open-end. Combed ring or compact yarn is the normal choice, because the smooth face of interlock shows every nep and thick place. Compact yarn has less hairiness, which helps pilling. Open-end yarn is rarely used for quality interlock; it feels harsher and looks duller.
Twist. Knitting yarn is spun with lower twist than weaving yarn; a twist multiplier (αe) of roughly 3.2 to 3.8 is typical for cotton, and it varies by spinner. Interlock absorbs most of the twist torque, but high-twist yarn still makes the fabric harder and can show as skew after washing.
Yarn evenness and lots. Because interlock is smooth and dense, small count variations show up as barre, horizontal bands of different shade or lustre. Use one yarn lot per order, and do not mix suppliers across feeders. See barre in knit fabric: causes and remedies.
Common mistake: pairing a jersey count with an interlock request. A 24/1 or 26/1 yarn that gives 170 to 180 GSM in single jersey will make a very heavy, board-like interlock on a 24 gauge machine. Start from interlock counts.
Knitting
Gauge and diameter
Gauge is the number of needles per inch on one bed. In interlock both beds have that gauge, so the effective needle density is double. In our register 24 gauge is by far the most used (618 entries), then 28 gauge (211), with a smaller group on 18 gauge (52) for coarser yarns. As in any knit, a finer count needs a finer gauge: too fine a yarn on a coarse gauge makes a loose fabric, and too coarse a yarn on a fine gauge causes needle damage, holes and stiffness.
Machine diameter sets the width. The most used diameter in our register is 36 inch (386 entries), then 34 inch (238), 38 inch (192) and 40 inch (65). Interlock runs on larger diameters than single jersey of similar width, because it finishes with more wales per centimetre.
Worked example. A 36 inch, 24 gauge interlock machine has 36 × 3.1416 × 24 = about 2,714 needles in the cylinder. Each face of the fabric shows one wale per cylinder needle. Our 40/1 cotton interlock on 24 gauge finishes at a median 165 cm open width, which means about 2,714 ÷ 165 = 16.4 wales per cm. If finishing pulled the fabric in to 17 wales per cm, the width would fall to about 160 cm; if it were stretched to 15.5 wales per cm, it would grow to about 175 cm, but the GSM would fall.
Stitch length, count and GSM
The weight of a knit is the weight of yarn in one square metre. For interlock, count the wales and courses per cm on one face. Every loop on that face has a partner loop on the other face, so the formula doubles:
GSM = (2 × courses per cm × wales per cm × stitch length in mm × yarn tex) ÷ 100, where tex = 590.5 ÷ Ne count, and courses and wales are counted on one face.
As a check, our 40/1 cotton interlock (tex 14.8) at 2.68 mm and 16.4 wales per cm needs about 16 courses per cm on one face to reach its median finished GSM of 210. That is a normal figure for interlock. You can try combinations with the knit GSM from stitch length calculator or the general GSM calculator; remember to enter the interlock form or double the single-face result.
The tightness factor, √tex ÷ stitch length in mm, works out at about 1.4 to 1.5 for the medians in our records (14 to 15 with stitch length in cm). That is lower than single jersey, because two layers of loops already give cover. A new construction far outside that band deserves a second look.
Count, gauge, stitch length and GSM from our records
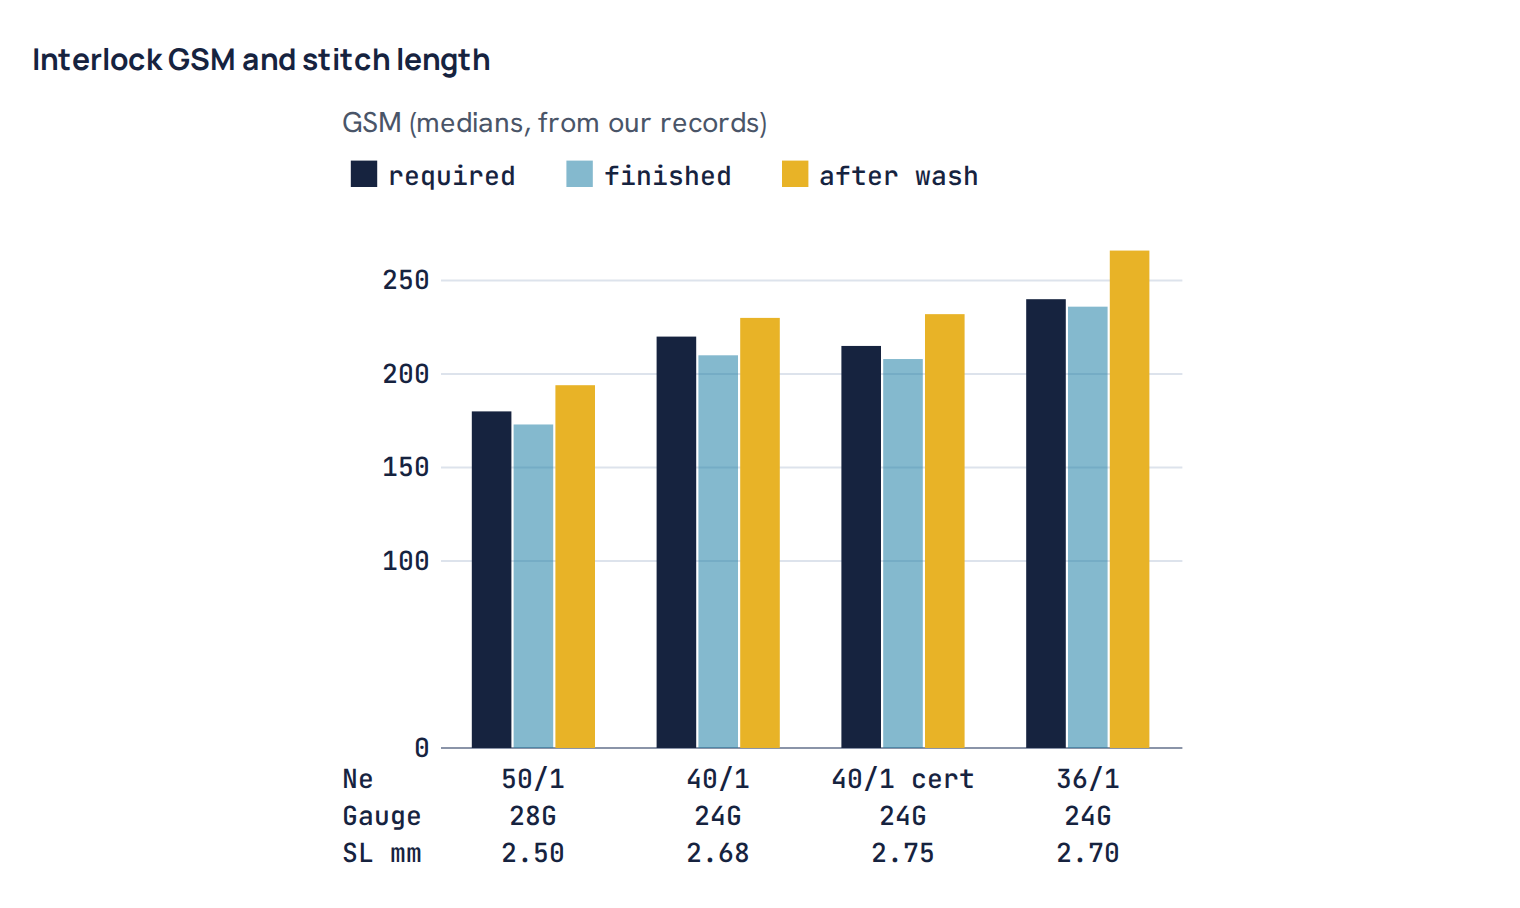
The table below shows the main 100% cotton interlock constructions in our register. Stitch length is in mm per loop, with the interquartile range (the middle half of entries) in brackets. Required GSM is what the buyer asked for; finished GSM is after dyeing and finishing; GSM after wash is after the dye-house wash test. Finished dia is open width.
| Yarn | Gauge | Entries | Stitch length, mm | Required GSM | Finished GSM | GSM after wash | Finished dia, cm |
|---|---|---|---|---|---|---|---|
| 40/1 cotton | 24G | 208 | 2.68 (2.64–2.70) | 220 | 210 (200–215) | 230 | 165 |
| 36/1 cotton | 24G | 104 | 2.70 (2.70–2.75) | 240 | 236 (231–240) | 266 | 172.5 |
| 50/1 cotton | 28G | 75 | 2.50 (2.50–2.55) | 180 | 173 (166–180) | 194 | 167 |
| 40/1 cotton, certified yarn | 24G | 29 | 2.75 (2.75–2.75) | 215 | 208 (205–213) | 232 | 187.5 |
Three things stand out. First, the stitch length band is very narrow: 2.68 to 2.75 mm on 24 gauge and 2.50 mm on 28 gauge, so new work should start there. Second, 36/1 and 40/1 run at almost the same stitch length on the same gauge, so the extra 20 GSM of the 36/1 fabric comes from the coarser yarn, not from a tighter knit. Third, finished GSM sits below required for every construction, and GSM after the wash test sits clearly above it. We come back to that in the section on hitting finished GSM.
Stitch length for the two needle sets. In interlock each feeder knits on its own set of needles, so in principle the two feeders can be set to different stitch lengths. Our register records a single stitch length per entry, not one value per needle set, so we cannot show the two separately. In normal practice both feeders are set to the same stitch length, and you should check that they really are the same: a difference between feeder 1 and feeder 2 shows as a fine stripe or uneven face and changes the fabric weight.
Needle set-out and cam arrangement
Before a trial, confirm the machine is set for interlock, not rib:
- Needle set-out. Long and short needles must alternate on both beds with no mistakes. One wrong needle shows as a continuous line down the fabric (a needle line).
- Gating. Dial and cylinder needles must be directly opposite (interlock gating), with a dial long needle facing a cylinder short needle.
- Cam tracks. At feeder 1 the cams knit the long needles and miss the short ones; at feeder 2 the opposite. On most machines this pattern repeats around the whole circle, so the number of complete courses per revolution is half the number of feeders.
- Dial height and timing. These affect loop formation, handle and stitch length. Record them and keep them the same from trial to bulk.
Elastane feeding in Lycra interlock
In Lycra interlock, bare elastane is fed from a positive feeder together with the ground yarn. It can be fed at every feeder (full feed) or only at some feeders, depending on the stretch and recovery the buyer wants. The elastane draft or tension must be the same at every elastane feeder; a difference shows as bars across the fabric and as uneven GSM. Lycra interlock relaxes much narrower and heavier than its cotton equivalent and must be heat-set before wet processing. Our register has 62 interlock entries with elastane, but too few of any one construction for a reliable median.
Machine settings to record
For every knitting trial, write down:
- Machine number, diameter, gauge, number of feeders and courses per revolution.
- Yarn count, type, lot and supplier at each feeder.
- Stitch length measured on the greige fabric, and if possible checked for feeder 1 and feeder 2 separately.
- Yarn input tension, and for Lycra the elastane draft and feed pattern.
- Cam and stitch settings, dial height and dial timing, and machine speed.
- Take-down tension or speed.
- Greige tubular dia, greige GSM and roll weight.
Greige inspection
Check the greige roll before it leaves the knitting floor: needle lines, drop stitches, holes, oil lines, barre and, on Lycra interlock, elastane breaks. Measure greige GSM and tubular dia after the roll has relaxed. Greige is usually lighter than finished, because the fabric shrinks in length in wet processing, so record greige values next to the finished results.
Dyeing and finishing route
Every interlock entry in our register is finished on an open-width route with stenter and compactor. The route below shows typical parameter ranges. Exact values depend on the dyes, chemicals, machine and shade, so treat them as a starting point. A short overview is in the interlock fabric dyeing and finishing flowchart. The full wet processes are in 100% cotton knit dyeing process, cotton elastane (Lycra) knit dyeing process and CVC fabric dyeing process.
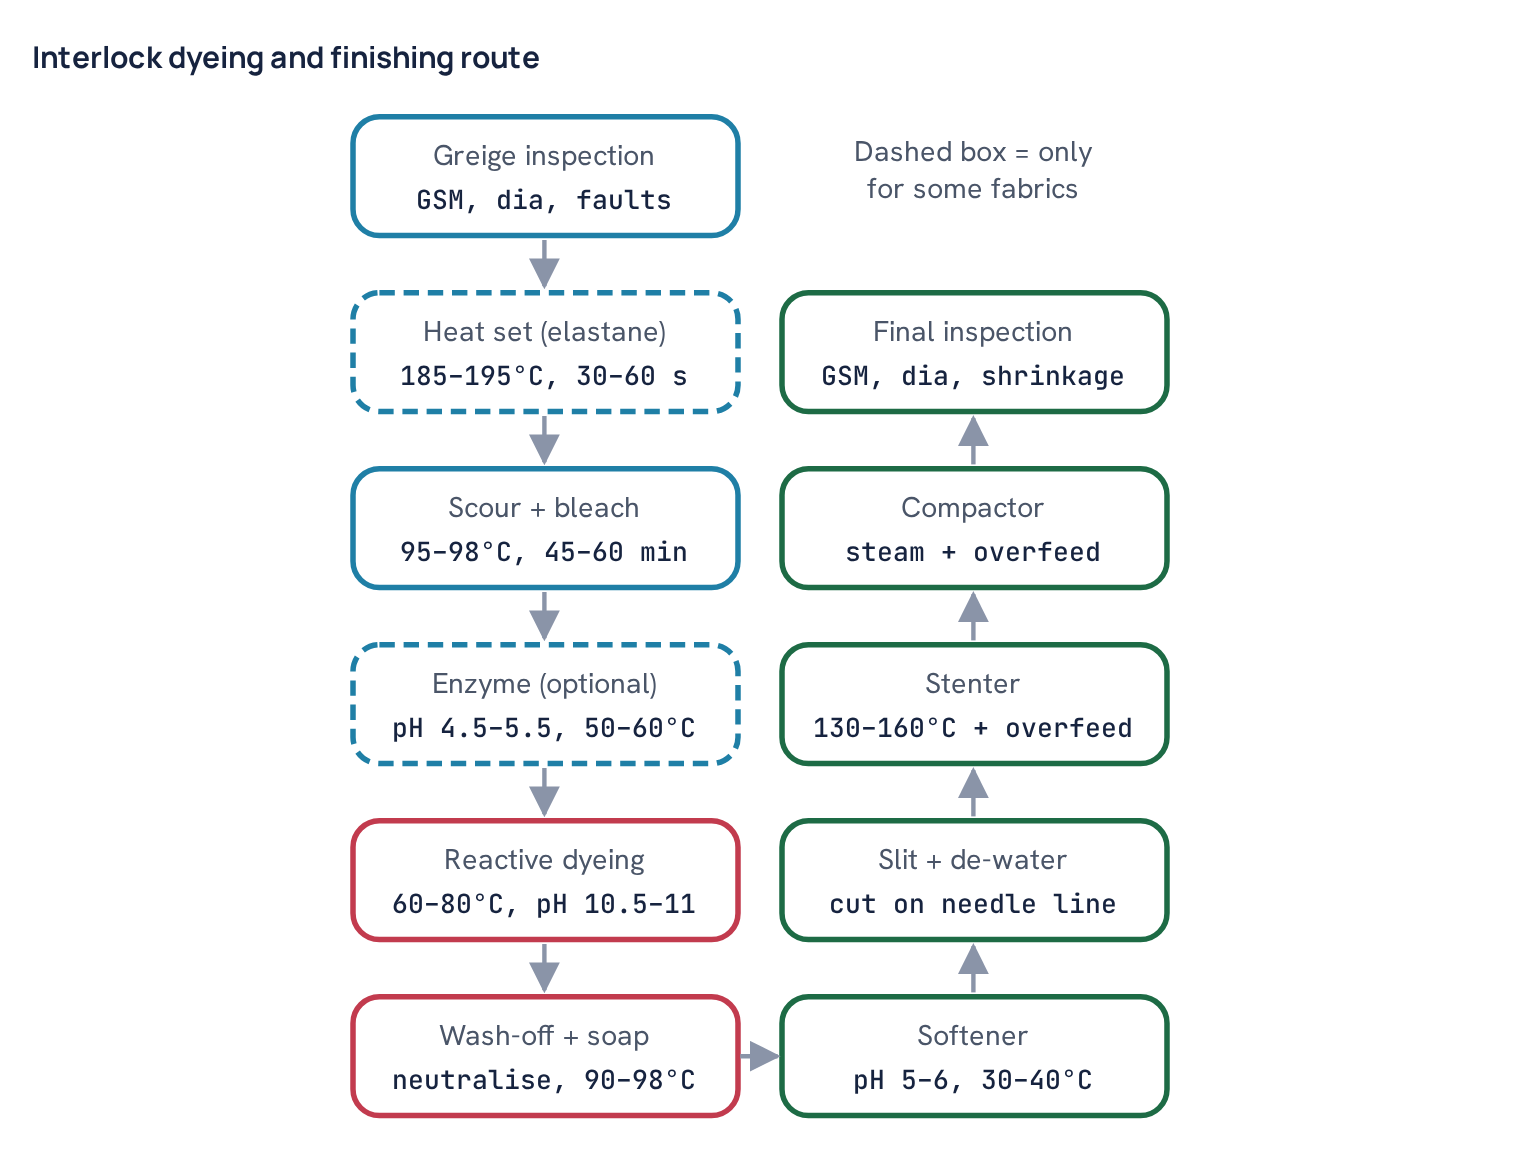
- Heat setting (elastane and some polyester blends). The greige fabric is set on the stenter, typically around 185 to 195°C for 30 to 60 seconds for cotton/elastane, at the planned width. This fixes the elastane so the fabric holds its width and does not crease or lose shape in dyeing. In our register 13% of all interlock entries carry a heat-set flag; for comparison, entries with elastane make up 62 of 887 (7%), and polyester blends without elastane another 138.
- Singeing and mercerising (some qualities). Singeing burns off surface fibres for a clean face; mercerising with strong caustic soda gives lustre, better dye uptake and a firmer fabric. On fabric, both come before or with pretreatment.
- Scouring and bleaching. Caustic soda, hydrogen peroxide, a stabiliser and a wetting agent, typically 95 to 98°C for 45 to 60 minutes, then hot rinse, neutralise and remove leftover peroxide. Interlock is dense, so give it good liquor flow and enough wetting agent to penetrate both layers.
- Enzyme (bio-polishing), if required. Acid cellulase at about pH 4.5 to 5.5 and 50 to 60°C for 45 to 60 minutes, then deactivate. It improves pilling but costs some weight and strength.
- Dyeing. Reactive dyes for cotton, with salt and alkali dosed in steps and fixation typically at 60°C for most vinyl sulphone and bifunctional dyes and up to 80°C for hotter types, at about pH 10.5 to 11. CVC and PC add a disperse dyeing step for the polyester at about 130°C. See how reactive dyes work and, for uneven results, level dyeing and uneven shades.
- Wash-off. Rinse, neutralise and soap near the boil. Dense interlock holds unfixed dye between its two layers, so a short wash-off shows later as poor wet rubbing and staining.
- Softener. Usually at 30 to 40°C and pH about 5 to 6. Choose a softener that does not reduce rubbing fastness or cause yellowing on whites.
- Slitting and de-watering. Slit along the marked needle line and de-water evenly.
- Stenter. Drying and width setting, typically 130 to 160°C for cotton, with overfeed to feed length back into the fabric. Lycra interlock must not be dried hotter than its heat-setting temperature. Every centimetre of width taken here comes off the GSM.
- Compactor. Steam and controlled overfeed compress the fabric in length, which reduces length shrinkage and raises GSM. For interlock this is the most important finishing step. Overfeed and steam are set from trials; record them.
Heavy, dense interlock is also prone to rope marks in jet dyeing, especially at high loads and with elastane; avoid shock cooling and see crease marks in knit dyeing.
Hitting finished GSM and width
What our records show
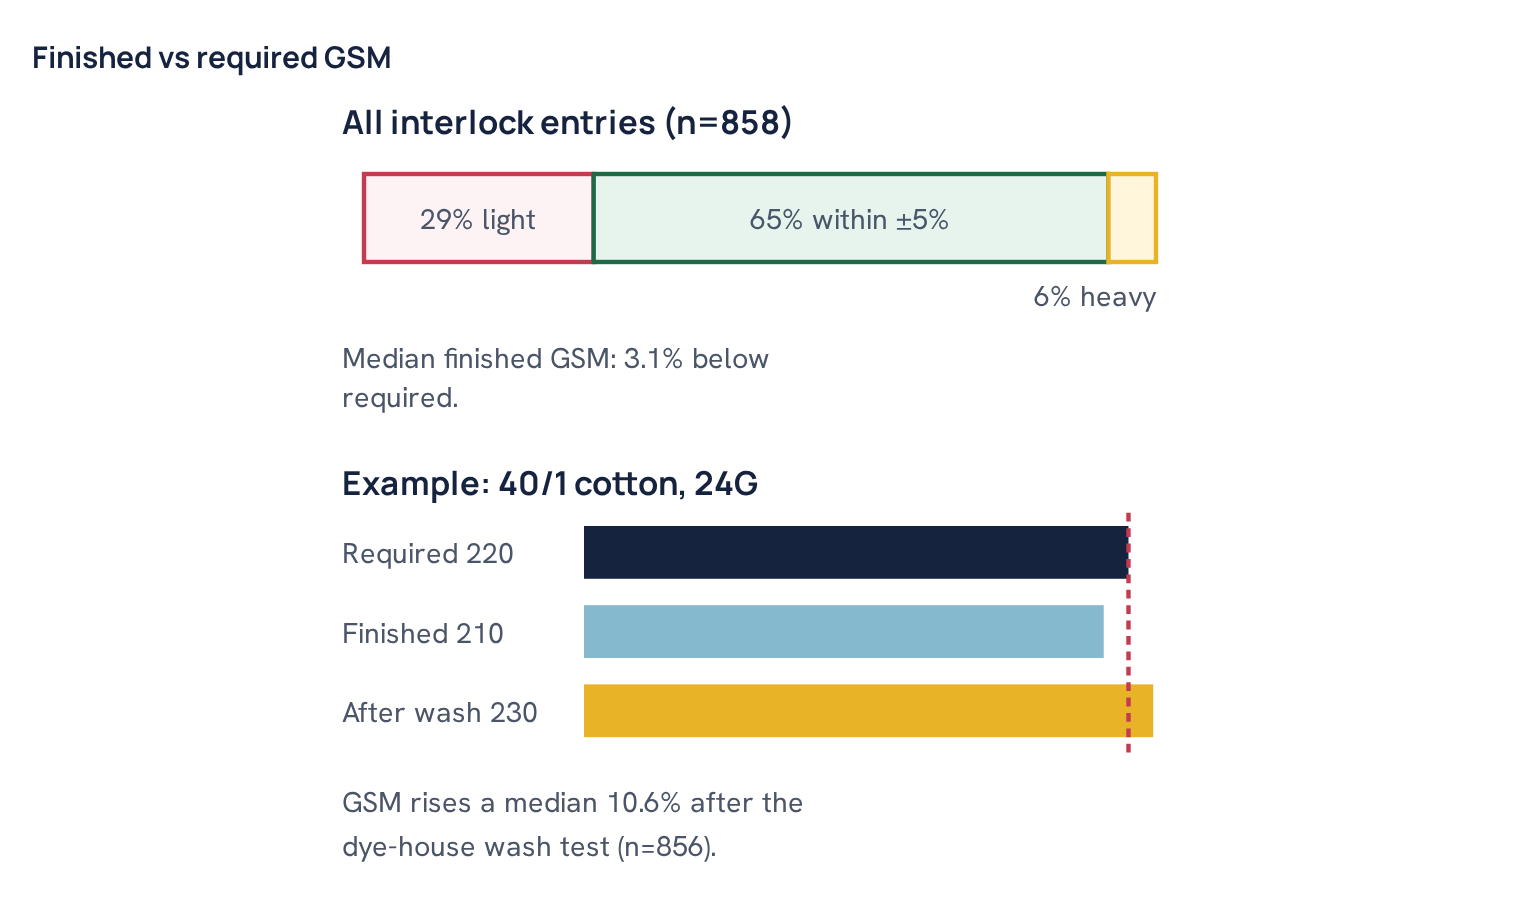
Interlock in our register finishes slightly light, but not as often as single jersey. Across 858 entries with both values, the median finished GSM is 3.1% below the required GSM. About 65% finish within ±5%, 29% finish more than 5% light and 6% finish more than 5% heavy. The bigger story is what happens in the dye-house wash test: GSM rises a median 10.6% (856 entries). That is a large change, and it tells you the fabric leaves the compactor with a lot of length still stretched in.
Why interlock finishes light, then gains in the wash
- Length stretched in during processing. Interlock is heavy, so it is pulled hard in length through the dyeing machine, the slitter and the stenter. If the compactor does not give that length back, the fabric is light and narrow-looped in courses when it leaves the floor.
- Stenter width stretch. Setting the width wide to meet the order makes the fabric thinner. The 40/1 cotton row has a 165 cm median width, while the certified-yarn row at a similar stitch length runs at 187.5 cm, and its GSM is a little lower and its width shrinkage higher (-5% against -3%). Width taken on the stenter tends to come back in the wash.
- Relaxation in the wash. When the dye house washes a sample, the loops relax, the courses close up and the GSM goes up. In our records the after-wash GSM is above the required GSM for every main construction: 230 against 220 for 40/1, 266 against 240 for 36/1, and 194 against 180 for 50/1.
- A dense two-layer fabric. Interlock needs more steam and overfeed than single jersey to relax fully.
The fabric has enough yarn in it; it simply has not relaxed. Shorten the stitch length to correct a light finished GSM and the fabric will be over weight after the customer’s first wash. Improve relaxation and compaction first.
Shrinkage in the dye-house wash test
The register’s shrinkage values come from the dye-house wash test. For the main cotton constructions the median is -7% in length and -3% in width for 36/1, 40/1 and 50/1. The certified-yarn 40/1 row runs at -5% in length and -5% in width, which matches its wider finishing. These are high figures against a common buyer limit of ±5%, and they agree with the 10.6% GSM rise: a fabric that shrinks 7% in length and 3% in width gains roughly 10% in weight. Plan more compactor overfeed for interlock than for jersey, and keep wet-processing tension low. You can estimate the effect on the garment with the fabric shrinkage calculator, and a fibre-by-fibre comparison is in our knit GSM and shrinkage by fibre study.
Spirality in the register is a median 2% for all four main constructions, which is low and expected for a balanced fabric.
Blends and Lycra interlock
Our table has enough entries per construction only for 100% cotton, so we give no blend medians. In general practice CVC and PC interlock shrink less and hold GSM better, because polyester does not swell in water. Lycra interlock pulls together strongly when free, so heat-set width, stenter width and compaction must be planned together.
How to plan greige GSM and dia
- Start from the table: stitch length and usual finished dia for the count and gauge.
- Expect a median finish about 3% below required, with a real chance of more than 5% light. Do not plan at the edge of tolerance.
- Knit a short trial, record greige GSM and dia, and send it through the full bulk route, including the compactor.
- Measure finished GSM, width and the GSM and shrinkage after the wash test. If finished GSM is low and after-wash GSM is high, the fix is compaction and relaxation, not knitting.
- Only if both finished and after-wash GSM are low, shorten the stitch length on both feeders slightly or use a coarser count.
- Write the greige-to-finished ratio for GSM and dia on the record sheet so the next order starts closer.
Common mistake: meeting a wide width order by stretching interlock on the stenter. The width and GSM look right at inspection, but the fabric shrinks in width and gains weight in the first wash, and both the shrinkage and the GSM test can fail.
Testing the developed fabric
Every development must pass the buyer’s tests before approval. We have 26 interlock lab reports that reached our desk. Many were sent because of a problem, so the fail rates are higher than in overall production. Use them to see where the risk lies, not as a production average.
| Test | Typical buyer requirement (varies by buyer) | Our lab reports (interlock) |
|---|---|---|
| Dimensional stability (shrinkage) | Often within ±5% L and W after the stated wash | 17 fails in 37 results; median after one wash L -3.1%, W -0.8% (n=20) |
| GSM | Often ±5% of the required GSM | 13 fails in 25 results |
| Spirality | Often 5% maximum after washing | 0 fails in 32; median 0.0%, max 2.2% |
| Bursting strength | A minimum in kPa set by the buyer | 2 fails in 20; median 283 kPa, range 128–500 (n=13) |
| Pilling | Often grade 3–4 minimum | 1 fail in 25; mostly pilling 4–5, fuzzing 4 |
| Colour fastness to rubbing | Often dry 4, wet 2–3 or 3 | 3 fails in 16; wet grades seen: 4 (8 times), 2–3 (4), 3 (3), 4–5 (1) |
| Colour fastness to water / perspiration / washing | Often 4 change, 3–4 staining | Water 1 fail in 14; perspiration 2 in 13; washing 0 in 11 |
| Fibre content | Within the label tolerance | 6 fails in 18 results |
| pH, light fastness, skew, appearance after wash | Buyer limits | No fails (4, 4, 5 and 5 results) |
| Phenolic yellowing | Grade 3 or better is common | 1 result, failed |
Four points stand out.
- Shrinkage and GSM are the problem tests. Shrinkage failed in 17 of 37 results and GSM in 13 of 25. That matches the register: interlock leaves finishing with length stretched in, then shrinks and gains weight. The median lab shrinkage after one wash, -3.1% in length and -0.8% in width, is lower than the dye-house wash test, because the lab test and the dye-house test are different methods; keep the two apart when you compare.
- Fibre content needs care. Six of 18 fibre analysis results failed. Fibre content fails usually mean the measured blend is outside the label tolerance, which is most likely with blends and elastane. Check yarn certificates, elastane feed and the declared composition before testing.
- Structure tests are strong. Spirality never failed (maximum 2.2%), skew and appearance after wash had no fails, bursting strength is high at a median 283 kPa, and pilling is mostly 4–5.
- Wet rubbing is the colour risk. Half the wet grades are 4, but 2–3 and 3 also appear, at common buyer limits; good soaping and the right softener help. The one phenolic yellowing result failed, so on whites check softener, packing and storage.
The test methods and fixes are covered in these guides:
- How to test shrinkage of knit fabric and shrinkage test fail: causes and remedies
- How to test GSM of knit fabric and GSM test fail: causes and remedies
- How to test spirality of knit fabric and spirality test fail: causes and remedies
- How to test bursting strength and bursting strength fail: causes and remedies
- How to test pilling (box and Martindale)
- Wet rubbing fastness fail: causes and remedies
Worked example. A 40/1 cotton interlock is required at 220 GSM. Our register median finishes at 210 GSM, 4.5% light, and rises to 230 GSM after the dye-house wash test with -7% length shrinkage. Before touching the 2.68 mm stitch length, raise compactor overfeed, reduce stenter width stretch and re-test both GSM and shrinkage.
Development record sheet and troubleshooting
Record sheet template
Use one sheet per trial and keep the request values and actual values side by side. Change one thing per trial so that you can see what made the difference.
| Stage | Record |
|---|---|
| Request | Buyer, style reference, required GSM and tolerance, finished width, composition, shade, wash care, test standard |
| Yarn | Count, type (combed/compact/organic/certified), supplier, lot, twist if known, elastane denier, blend ratio |
| Knitting | Machine no., diameter, gauge, feeders, courses per revolution, needle set-out check, stitch length (measured; feeder 1 and feeder 2 if possible), yarn input tension, elastane draft and feed, dial height and timing, take-down, speed |
| Greige | Greige GSM, tubular dia, roll weight, faults found |
| Heat set / singe / mercerise | Temperature, time or speed, set width, overfeed, as applicable |
| Wet process | Machine, batch load, pretreatment recipe, enzyme yes/no, dye recipe, fixation temperature and pH, wash-off, softener |
| Stenter | Temperature, speed, set width, overfeed |
| Compactor | Overfeed, steam, temperature, exit width |
| Finished | Finished GSM, open width, GSM after wash test, shrinkage L/W, spirality, shade result |
| Lab tests | Each result against requirement, pass/fail |
| Decision | Approved / adjust; what will change in the next trial, and why |
Troubleshooting
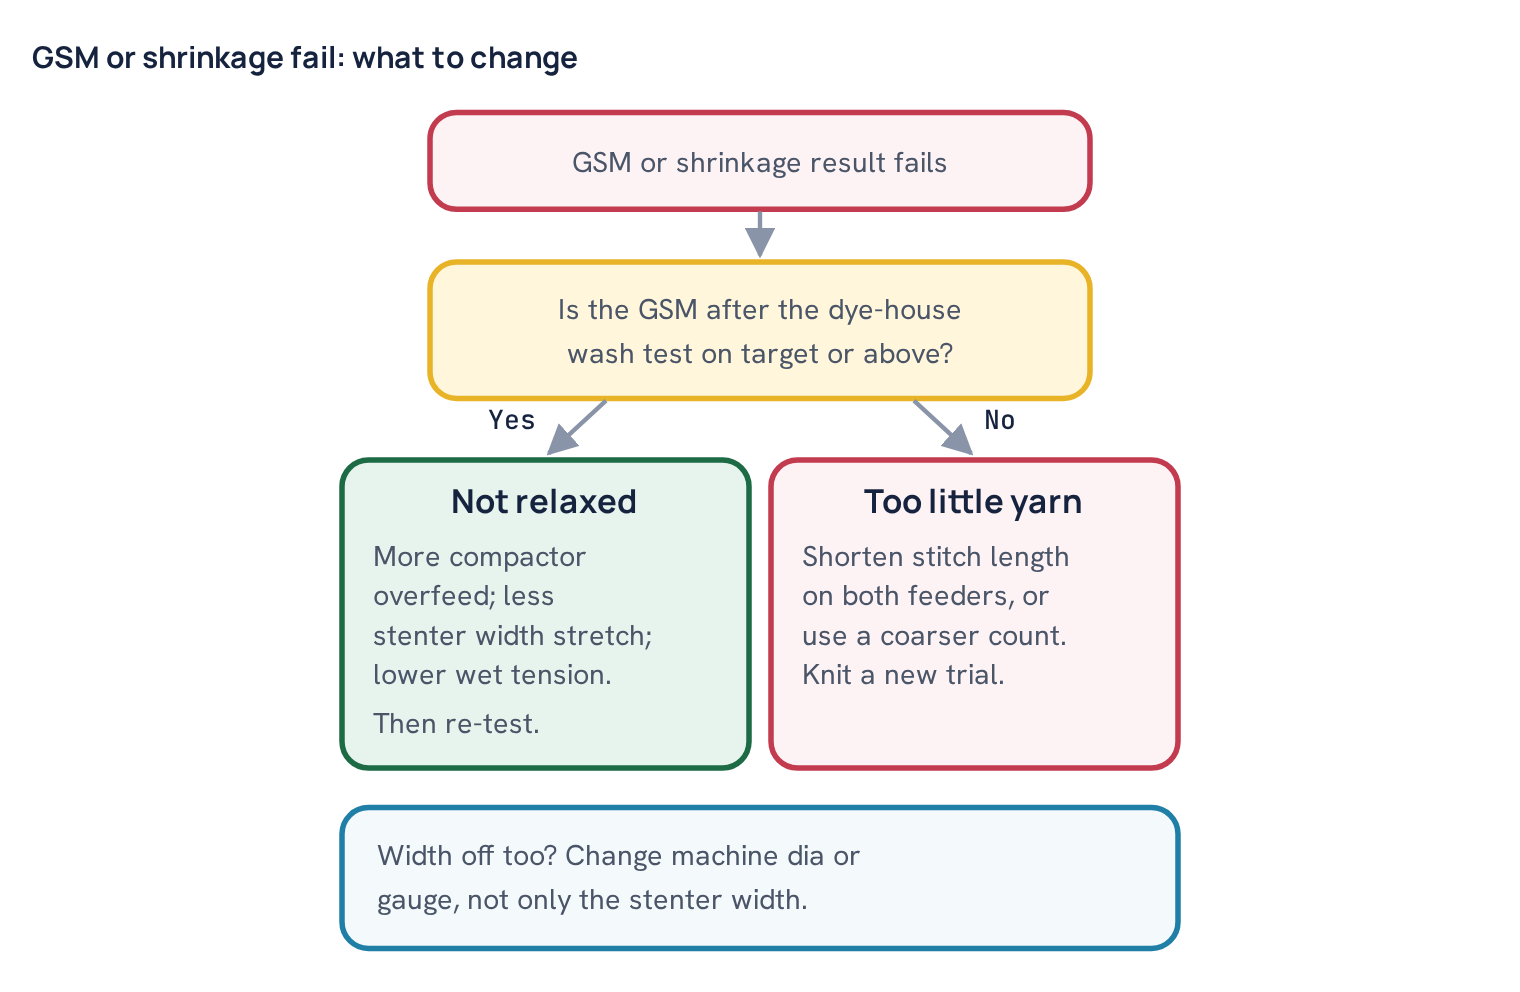
Most interlock problems in our data are GSM and shrinkage, with one root. The path below separates a finishing fix from a knitting fix.
| Problem | Likely cause | What to change |
|---|---|---|
| Finished GSM low, after-wash GSM on target or high | Fabric not relaxed; length stretched in; stenter too wide | More compactor overfeed and steam, more stenter overfeed, less width stretch |
| Finished and after-wash GSM both low | Stitch length too long or count too fine | Shorten stitch length on both feeders slightly, or use a coarser count |
| GSM too high, fabric boardy | Count too coarse for the gauge; stitch length too short; over-compacted | Finer count or longer stitch length; reduce compaction |
| Length shrinkage high | Too little compaction; high tension in dyeing and stenter | Raise compactor overfeed; lower tension; more stenter overfeed |
| Width shrinkage high or width grows | Stretched wide on stenter, or over-narrowed in compaction | Set width closer to the relaxed width; change machine dia if needed |
| Vertical line down the fabric | Wrong or damaged needle; set-out error | Check long/short needle sequence; replace needle |
| Fine stripe or uneven face | Different stitch length on feeder 1 and feeder 2; uneven yarn tension | Measure and equalise both feeders |
| Barre | Mixed yarn lots or counts; uneven elastane tension | One yarn lot per order; equalise feeder and elastane tension |
| Lycra interlock narrow, curly or creased | No heat set, or set too low or too narrow | Heat set at the right temperature and width before wet processing |
| Fibre content fail | Blend or elastane share differs from the label | Check yarn certificates, elastane feed and declared composition |
| Wet rubbing low | Poor wash-off in dense fabric; deep shade; unsuitable softener | Longer or hotter soaping; review recipe depth and softener |
| Yellowing on whites | Unsuitable softener; packing or storage | Non-yellowing softener; check packing materials and storage |
Start from proven count, gauge and stitch length pairs, check the needle set-out and both feeders, expect the fabric to finish slightly light and gain about a tenth in the wash, and put your effort into relaxation and compaction. Record every trial so the next one starts closer.
Questions
What stitch length is used for 40/1 cotton interlock?
In our development records the median is 2.68 mm on a 24 gauge machine, for a required GSM of 220. Our register records one stitch length per entry; both feeders are normally set the same.
Why is interlock smooth on both sides?
Interlock is two 1×1 ribs knitted by two feeders on long and short needles of the dial and cylinder. The second rib fills the gaps of the first, so each side shows only face loops and the back loops are hidden inside.
Why does interlock gain GSM after washing?
It leaves the compactor with length still stretched in. When it relaxes in the wash it shrinks, in our records a median -7% in length and -3% in width, and GSM rises a median 10.6%.
Which gauge is used for interlock?
In our register 24 gauge is the most common, used with about 36/1 to 40/1 cotton, then 28 gauge with finer yarn such as 50/1. A smaller group runs on 18 gauge for coarser yarns.
What are the most common interlock test fails?
In our interlock lab reports, shrinkage failed in 17 of 37 results and GSM in 13 of 25, and fibre content in 6 of 18. Spirality did not fail in 32 results.
Textile engineer with 14+ years in dyeing and fabric development. He writes every guide on Dyeing Solution from real production work. Full profile